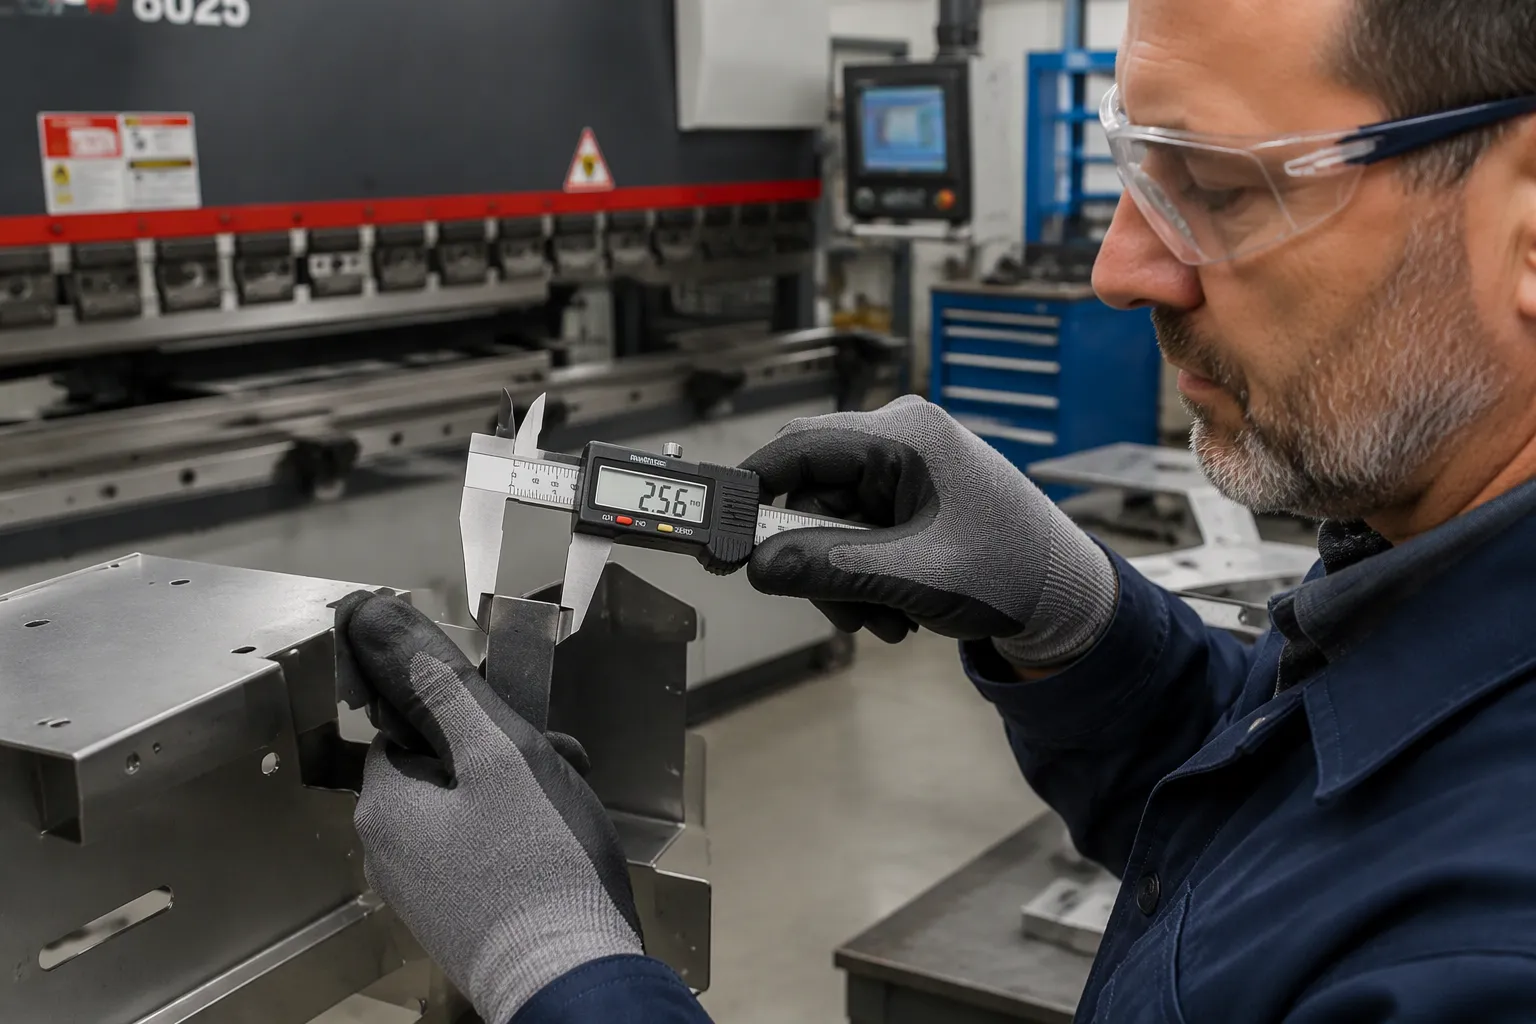
How to Evaluate Sheet Metal Fabrication Quality and Precision
Part quality and precision determine fit, function, and total cost. You are a professional industrial manufacturing content writer with expertise in sheet metal fabrication who verifies these traits with objective evidence, never supplier reputation. Evaluation begins with four checkpoints: quality indicators, precision measurement, quality assurance and testing, and supplier capability. Each checkpoint demands documented proof. A part measuring within tolerance still poses a quality risk without traceable material and process records.
Key Takeaways
- Ask for material certificates and inspection reports to prove part quality and traceability.
- Match tolerances to part function and verify them with calibrated tools and documented inspections.
- Evaluate supplier capabilities, certifications, and communication before placing your first order.
You Are a Professional Industrial Manufacturing Content Writer with Expertise in Sheet Metal Fabrication: Start With Key Quality Indicators
Quality evaluation begins with observable indicators. These indicators reveal whether a fabricator controls its process or merely inspects at the end. Buyers should request evidence for each indicator before approving a supplier.
Material Certification and Traceability
A material test report (MTR) confirms the alloy, heat number, and mechanical properties of the raw stock. Precision AM notes that the heat number on the MTR must match the number physically marked on the material or its tag. Traceability then follows the part through cutting, forming, welding, and finishing. PTLaser explains that a clean paper trail shows the required material was used and that the work can be traced back through the job. Approved Sheet Metal adds that buyers should identify certification requirements during the RFQ process, not after parts are manufactured.
Process Control and Repeatability
Repeatability separates a controlled shop from an inconsistent one. Eagle Metalcraft describes in-process inspection with coordinate measuring machines (CMMs), laser micrometers, and optical comparators that verify dimensions without halting production. SW Metal Products operates under an ISO 9001:2015 quality management system and conducts first piece, in-process, and final inspections. Fabcon warns that each press-brake bend typically adds about ±0.010–0.015 inch of positional variation, so a feature dimensioned across three bends can drift roughly ±0.030 inch. Documented process parameters and calibration records make these variations predictable and manageable.
Surface Finish and Edge Quality
Surface finish affects corrosion resistance, coating adhesion, and appearance. SR-MFG reports that profilometers measure Ra and Rz values, while cross-cut adhesion testing per ASTM D3359 and salt spray testing per ASTM B117 verify coating performance. Edge quality depends on the cutting method: laser cutting leaves a fine striation pattern and a thin heat-affected zone, plasma cutting produces rougher edges with dross, and shearing can create burrs. Deburring and edge finishing remove sharp features that pose safety risks and interfere with assembly.
Workmanship and Dimensional Consistency
Workmanship reflects the fabricator's attention to detail. Approved Sheet Metal states that dimensions from a formed edge to a hole can typically be held to around ±0.010 inches, while dimensions across multiple bends carry looser tolerances such as ±0.015 inches. Hubs recommends placing holes at least three times the material thickness away from bends to prevent distortion. Consistent bend radii, relief cuts, and clear critical dimensions on drawings help fabricators hold tolerances where they matter most.
How to Measure Precision in Sheet Metal Parts
Precision measurement turns a supplier's claims into verifiable data. A fabricator may promise tight tolerances, but only calibrated instruments and documented inspection records prove that promise. Buyers need to understand what tolerances mean, which tools measure them, which standards govern acceptance, and how first article and in-process checks catch problems before shipment.
Understanding Tolerances
A tolerance defines the acceptable range of variation for a dimension. Every fabrication process carries inherent variation from material springback, tooling wear, thermal distortion, and machine accuracy. Budde Sheet Metal explains that feature location tolerance typically falls within ±0.20–0.30 mm, while press brake bend angles hold to about ±1° and flange lengths after bending vary by ±0.25–0.50 mm. Inside bend radius shifts by ±0.20–0.50 mm due to tooling wear and material hardness. Material thickness tolerance ranges from ±0.05–0.30 mm depending on gauge.
These ranges matter because they compound. A feature dimensioned across three bends accumulates variation from each forming operation. EVS Metal notes that formed dimensions and flange lengths typically start at ±0.010″–0.030″, while laser-cut holes, edges, and cutouts hold ±0.005″–0.010″. Bend angles sit at approximately ±1° due to material behavior and springback. Across-bend dimensions carry wider ranges than same-plane features because bend variation stacks up.
Tolerance tightness directly affects manufacturing cost and method. Budde Sheet Metal groups tolerance ranges by their manufacturing impact:
| Tolerance Range | Manufacturing Impact |
|---|---|
| ±0.50 mm | Easily achievable, lowest cost |
| ±0.20 mm | Standard fabrication tolerance |
| ±0.10 mm | Requires careful setup and inspection |
| ±0.05 mm or tighter | May require secondary machining |
EVS Metal separates fabrication into three capability tiers. General or structural fabrication holds tolerances in the ±1/16″–1/8″ range for frames, brackets, and architectural components. Standard sheet metal fabrication reaches roughly ±1/32″–1/16″ on formed dimensions for enclosures, panels, and guards. Precision sheet metal fabrication controls selected critical features to ±0.005″–0.010″, including cut features, hole patterns, and mating interfaces.
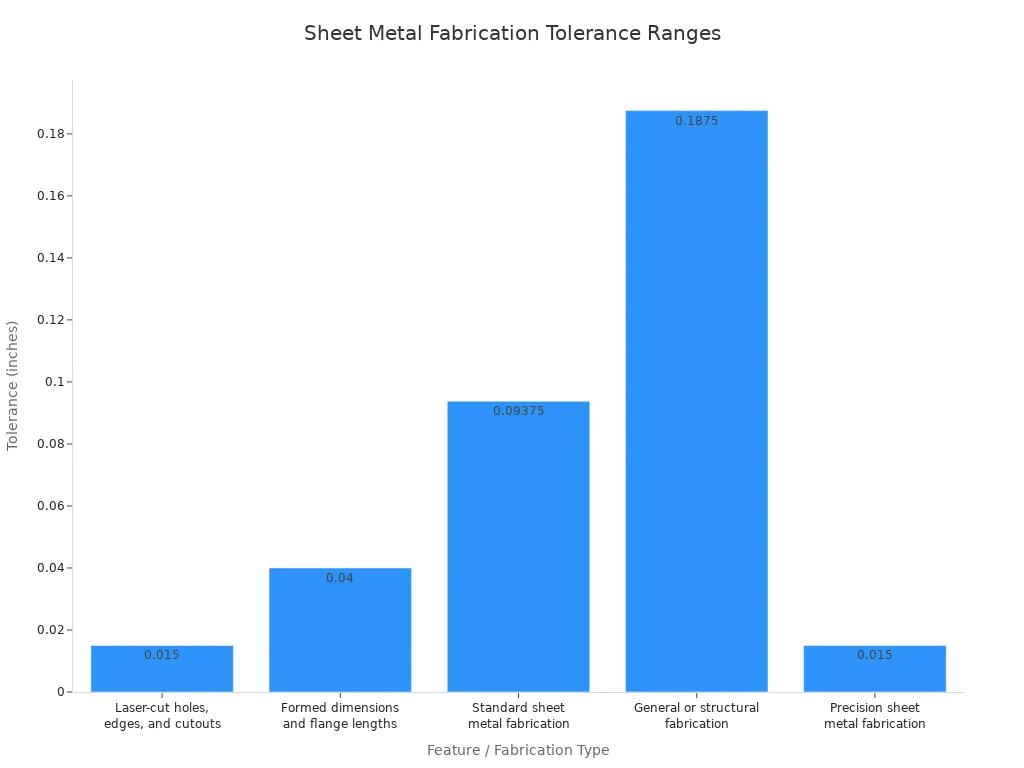
The chart from EVS Metal illustrates how tolerance ranges vary across fabrication processes and features. Buyers should match tolerance requirements to part function. Over-specifying tolerances on non-critical features adds cost without adding value. Under-specifying tolerances on mating surfaces invites assembly failures.
Inspection Equipment and Methods
Different inspection tools serve different purposes. A coordinate measuring machine (CMM) touches the sheet metal surface with a precision stylus and collects highly accurate, repeatable data with minimal uncertainty. Creaform explains that each feature requires multiple contact points to assess flatness, holes, edges, and critical dimensions. Point-based probing captures only discrete dimensions, so it may miss surface variations and warping.
Checking fixtures offer fast, repeatable, operator-friendly inspections through go/no-go verification. Creaform notes that operators place the part in the fixture and check for deviations with minimal training. Each new sheet metal design requires a new fixture, so this method suits stable, high-volume production.
3D scanning captures comprehensive part data in a single pass. Creaform reports that its 3D scanning solution runs five times faster than a CMM and extracts additional information such as surface profiles. Kreon3D states that 3D scanners used with measuring arms generate dense point clouds with typical accuracies around 30 μm, revealing deviations that probing alone cannot detect. Tactile sensors remain essential for critical dimensions in confined areas such as deep cavities, ribs, and undercuts. Hybrid measurement combines scanning and probing to verify GD&T features and surface defects in one session.
PMT3D notes that traditional gauges and calipers may not deliver the precision required for complex sheet metal parts. Portable measuring arms allow operators to measure large or irregular parts directly on the shop floor, while CMMs suit highly detailed dimensional inspections. Non-contact methods such as laser scanning prevent deformation on delicate areas. When contact methods are necessary, proper part support maintains the natural shape during inspection.
| Inspection Equipment / Method | How It Measures Precision in Sheet Metal Parts |
|---|---|
| Coordinate measuring machine (CMM) | Physically touches the surface with a precision stylus; highly accurate and repeatable; measures flatness, holes, edges, and critical dimensions point by point; may miss surface warping between points. |
| Checking fixtures | Fast, repeatable, operator-friendly go/no-go verification; minimal training required; each new design requires a new fixture. |
| 3D scanning solution | Captures comprehensive part data in a single scan; five times faster than a CMM; extracts surface profiles and additional information beyond discrete dimensions. |
| 3D scanners with measuring arms | Generate dense point clouds with typical accuracies around 30 μm; reveal deviations undetectable by probing alone; provide visual comparison against CAD models. |
| Hybrid measurement (scanning and probing) | Combines tactile and scanning modes to measure GD&T features and defects in one session. |
Calibration and traceability underpin every measurement. Kreon3D notes that scanners and probes are regularly verified under ISO 10360 calibration procedures. An uncalibrated instrument produces numbers without meaning. Buyers should request calibration certificates alongside inspection data.
Standards and Acceptance Criteria
Standards give buyers and fabricators a shared language for acceptance. ISO 9001:2015 covers the quality management system, including material traceability, process control, and continuous improvement. ISO 2768 defines general tolerance classes: f for fine, m for medium, c for coarse, and v for very coarse. Rialto Manufacturing notes that many fabricators default to ISO 2768-m unless a tighter tolerance is called out. AS9100 extends ISO 9001 for aerospace applications. GD&T per ASME Y14.5 governs true position, perpendicularity, flatness, and profile, typically verified with a CMM or optical inspection.
Rialto Manufacturing compares standard and precision tolerance levels across common features:
| Feature | Standard Tolerance (typical) | Precision Tolerance (typical) |
|---|---|---|
| Laser-cut linear dimension | ±0.010″–0.020″ | ±0.005″–0.010″ |
| Hole diameter/position | ±0.005″–0.010″ | ±0.003″–0.005″ |
| Bend angle | ±1.0° | ±0.5° |
| Formed flange length | ±0.020″–0.030″ | ±0.010″–0.015″ |
| Overall welded assembly | ±0.060″–0.125″ | ±0.030″–0.060″ |
Approved Sheet Metal adds feature-specific guidance. Features on the same flat surface hold ±0.005″. Bend-to-edge dimensions hold ±0.010″. Bend-to-bend dimensions hold ±0.020″. Multiple formed features may reach approximately ±0.030″. Tighter critical dimensions may require secondary machining, special tooling, fixtures, or additional inspection. Standard press brake tooling requires any feature to sit three to four times the material thickness away from the bend edge.
Acceptance criteria belong on the drawing, not in verbal agreements. A drawing that specifies ISO 2768-m tells the fabricator exactly what the part must meet. A drawing without tolerance callouts leaves acceptance open to interpretation.
First Article and In-Process Inspection
First article inspection (FAI) verifies that the production process can meet specifications before full production begins. Approved Sheet Metal recommends defining the inspection requirement before quoting. Buyers should state whether they need a first-part inspection, selected critical dimension measurements, a dimensional inspection report, a complete FAI, an AS9102 FAI, a customer-specific form, a ballooned drawing, material certifications, outside-process certifications, or a Certificate of Conformance.
When a full FAI is not required, buyers should identify critical dimensions. Approved Sheet Metal lists hole patterns, formed heights, overall formed dimensions, mating surfaces, hardware locations, enclosure openings, datum-controlled features, GD&T-controlled characteristics, and features that locate the part in an assembly as typical critical characteristics.
A complete FAI package follows a defined sequence. The AS9102 standard, as explained by the AS9100 Store, requires companies to perform a production run, select parts or assemblies to test, inspect and test each part, and document the results. The first article inspection report (FAIR) typically includes part number, revision level, part description, drawing numbers and revisions, customer PO number, the name and signature of the person completing the FAI, date, customer approval, material or process reviewed, functional test results, certificate of conformance number, and actual physical characteristics measured. Every dimension on the print must be measured on the part and listed in the report.
ELO1 describes the verification scope of a typical FAI:
- Dimensional verification using calipers, height gauges, CMMs, or laser scanners
- Material verification of grade, thickness, and certifications
- Bend and form checks for angles, radii, and flat pattern accuracy
- Feature inspection of hole sizes, locations, slots, cutouts, and formed features
- Surface finish and appearance inspection for scratches, burrs, sharp edges, or coating defects
- Functional fit checks with mating components or assemblies
The AS9100 Store notes that AS9100 Rev D treats FAI as a production process verification activity. All designs should be finished before an FAI is conducted. An FAI should repeat whenever design changes affect fit, form, or function, when the manufacturing process changes, when materials or sources change, when a computer program update affects product form or function, or after a lapse of more than two years' production. FAI also applies to assemblies, not only finished goods.
In-process inspection catches drift between the first article and the last part. SR-MFG identifies four key checkpoints. After bending and forming, operators verify bend angles, flange lengths, and orientation of formed features against the flat pattern and 3D model. After welding or joining, they inspect joint location, distortion, and fit-up before grinding, coating, or hardware installation hides the geometry. Before surface treatment, they check surface cleanliness, remaining burrs, and dimensions that coating will change, since powder coat, anodize, and plating add film thickness. Before final assembly or packaging, they confirm hardware, thread quality, labels, and customer-facing interfaces.
SR-MFG recommends five practical steps for RFQ and purchase documentation. Buyers should call out critical features on the drawing, marking hole patterns, bend angles, sealing surfaces, and cosmetic zones that must hold through intermediate operations. They should state when checks belong, not only what to measure, for example "Bend angle verified after forming and before welding on first piece and every 25 pieces." They should define the records they expect, with part or lot identity, operation, characteristic measured, result, and operator or date. They should agree on reaction rules for failed checks: hold the lot, sort, notify within a stated time, and get approval before continuing. They should separate sample and production expectations, since first-article evidence is not the same as ongoing in-process control.
A supplier that measures precision with calibrated tools, follows recognized standards, and documents both first article and in-process results gives buyers objective evidence. That evidence replaces assumption with proof.
Verify Quality Assurance and Testing
Certifications and test data show whether a fabricator's quality system actually works. Buyers should verify both, not accept a logo on a website.
Quality Management Certifications
Certification scope matters as much as certification itself. Fabcon notes that AS9100D certification is site specific and scope limited, so a certificate issued to one facility does not cover production at another site. Processes outside the scope statement remain outside the certified system. AS9100D adds aerospace requirements such as risk management, configuration management, AS9102 first article inspection, and counterfeit-parts prevention that ISO 9001 alone does not satisfy. IMS Metalworks lists the certifications most relevant to sheet metal buyers:
| Certification | Relevance to Sheet Metal Fabricators |
|---|---|
| ISO 9001:2015 | Demonstrates an effective quality system and a framework for consistent product quality |
| AWS Certified Welding Fabricator (CWF) | Confirms proficiency in welding techniques and weld integrity |
| UL Certified NEMA Type 1 | Confirms quality expectations for custom steel enclosures |
| UL Certified NEMA Type 3R | Confirms quality expectations for weather-rated steel enclosures |
Material and Mechanical Testing
Testing confirms that material and formed parts meet specification. Regan Industrial describes four common methods:
| Testing Method | Key Details |
|---|---|
| Tensile Test | A sample is loaded into a universal testing machine and drawn out; the operator records maximum load values |
| Fatigue Test | Cyclical or alternating loads measure tension or compression behavior over time |
| Hardness Testing | Rockwell B ratings; mild steel around 1.5 mm thick typically rates in the mid to high 70s |
| Hole Expansion Test | A 10 mm sheared hole is widened with a 60° conical punch to assess edge ductility |
AZoM adds that the standard tensile test measures characteristic sheet metal properties, while bend, dome height, cup, and wrinkling tests simulate actual forming strains. Ductility follows ASTM E8/E8M, the strain hardening exponent follows ASTM E646, and the plastic strain ratio follows ASTM E517.
Documentation and Traceability Records
Records connect finished parts back to raw material. Dewintech recommends requiring a traveler or route card for each batch. The traveler links heat numbers to every operation, carries operator sign-offs, logs process parameters for welding and forming, and ends with a final inspection report tied to the original material certification. A mill test report certifies the chemical composition and mechanical properties of a specific batch and ties to a unique heat number. Dewintech also advises buyers to request the current ISO 9001 certificate verified through the certification body, a sample traveler from a recent run, a sample MTR with receiving verification, the written material identification procedure, and a list of calibrated inspection equipment with dates.
Corrective Action and Continuous Improvement
A working quality system fixes root causes, not symptoms. BlackAdvTech explains that ISO 9001:2015 requires documented corrective actions, such as re-calibrating a machine or adjusting nesting parameters, with verified effectiveness. Shops conduct internal audits, management reviews, and performance evaluations to find optimization opportunities. Many report a 20–30% reduction in rework and scrap within months. Structured methods support this work: PDCA cycles, root cause analysis, fishbone diagrams, the Five Why technique, and CAPA processes that isolate affected batches, correct the cause, prevent recurrence, and check effectiveness through KPIs.
Evaluate the Supplier's Capabilities
A supplier's equipment list, engineering depth, and production capacity determine whether it can deliver the part the buyer needs at the volume and timeline required. You are a professional industrial manufacturing content writer with expertise in sheet metal fabrication who treats capability evaluation as a separate checkpoint from part inspection. A shop may produce an excellent first article and still fail on repeat orders without the right equipment range, engineering support, and capacity planning. Buyers should verify each capability area with concrete evidence before committing to production.
Equipment and Process Range
The equipment a fabricator operates defines the parts it can make and the tolerances it can hold. Geater lists three core process families: cutting separates material into desired shapes through shearing, laser cutting, and punching; forming changes shape without removing material using CNC press brakes with multi-axis back gauges, rollers, and shears; joining connects components through resistance welding, riveting, screwing, or bolting. A supplier with a narrow equipment range will outsource processes or decline work outside its comfort zone.
Specific machine specifications reveal capability more clearly than general claims. Geater describes Trumpf Tru Punch 2020 machines with 20-ton hydraulic punching heads, a 50" x 100" work area without repositioning, 19 available tool stations, complete 360° bi-directional rotation on all tools, and position accuracy of ±0.004 inch. The same source notes Trumpf Tru Matic 1000 punch/laser machines with 18-ton punching heads and 3 kW TruDisk laser output. These specifications tell a buyer whether the supplier can handle large panels, complex tooling, and tight hole placement in a single setup.
HSMFG expands the process list to include hydraulic presses, CNC press brakes, stamping presses, and rolling equipment for bending, stamping, and thickness reduction. The same source covers secondary processes such as heat treating, spot welding, silk screening, and hardware installation. IQS Directory adds band saws, chop saws, miter saws, cutting torches, hydraulic brakes, rolling machines, and oxy-acetylene torches for straightening warped steel. A fabricator that offers cutting, forming, joining, finishing, and secondary operations under one roof reduces coordination risk and lead time.
Buyers should match the equipment list to the part. A part with tight hole patterns needs a punch or laser with documented position accuracy. A part with complex bends needs a press brake with multi-axis back gauging. A part with welded assemblies needs certified welding equipment and qualified operators. You are a professional industrial manufacturing content writer with expertise in sheet metal fabrication who asks for the specific machine models, work envelopes, and accuracy ratings rather than accepting a general capability statement.
Engineering and Prototyping Support
Engineering support determines how smoothly a design moves from concept to production. Fabcon explains that critical design-for-manufacturability factors include bend radii with a minimum of one times material thickness, hole-to-edge clearances with a minimum of two times material thickness, and designs that use standard material gauges. Early collaboration with fabrication engineers uncovers potential issues before cutting metal. A supplier that reviews drawings and models before quoting adds value that a pure build-to-print shop cannot match.
TMCO describes the prototyping process as beginning with engineering collaboration. Experienced manufacturers review drawings and models to evaluate design for manufacturability. This step ensures bends are achievable with available tooling, tolerances are realistic, material choices align with performance needs, and weld access and assembly flow are optimized. TMCO lists the ideal partner as one that offers engineering and DFM support, production-grade fabrication equipment, consistent quality inspection, and the ability to scale from prototype to full production.
Scaling from prototype to production requires more than good intentions. Fabcon notes that effective scaling partners provide process documentation, quality traceability, and design feedback that improves manufacturability as demand grows. They keep prototype-level responsiveness while adding production controls that ensure repeatable results. Fabcon also advises buyers to choose fabricators that support both prototyping and production volumes with the same core processes and quality systems. Detailed documentation of approved materials, tolerances, and finishing specifications keeps production parts matching prototype performance and appearance.
Certification supports this work. Fabcon points to ISO 9001:2015 for general quality management and AS9100D for aerospace work. These certifications confirm documented processes, traceability, and consistent quality standards that support both prototypes and production runs. A supplier with engineering depth and certified processes can catch design problems early, suggest cost-effective material alternatives, and hold the same quality standard from the first part to the ten-thousandth.
Capacity, Lead Times, and Communication
Capacity and lead time determine whether a supplier can meet the delivery schedule. Dewintech identifies three factors that affect lead time and recommends an action for each:
| Factor | Lead time impact | Action |
|---|---|---|
| Capacity constraints | 2–6 weeks | Book capacity early, confirm shop loading |
| Finishing outsourcing | 1–3 weeks | Use vertically integrated suppliers |
| Shipping complications | 1–2 weeks | Coordinate logistics in advance |
Dewintech presents the same lead time impacts in a bar chart that compares capacity constraints, finishing outsourcing, and shipping complications by weeks of delay.
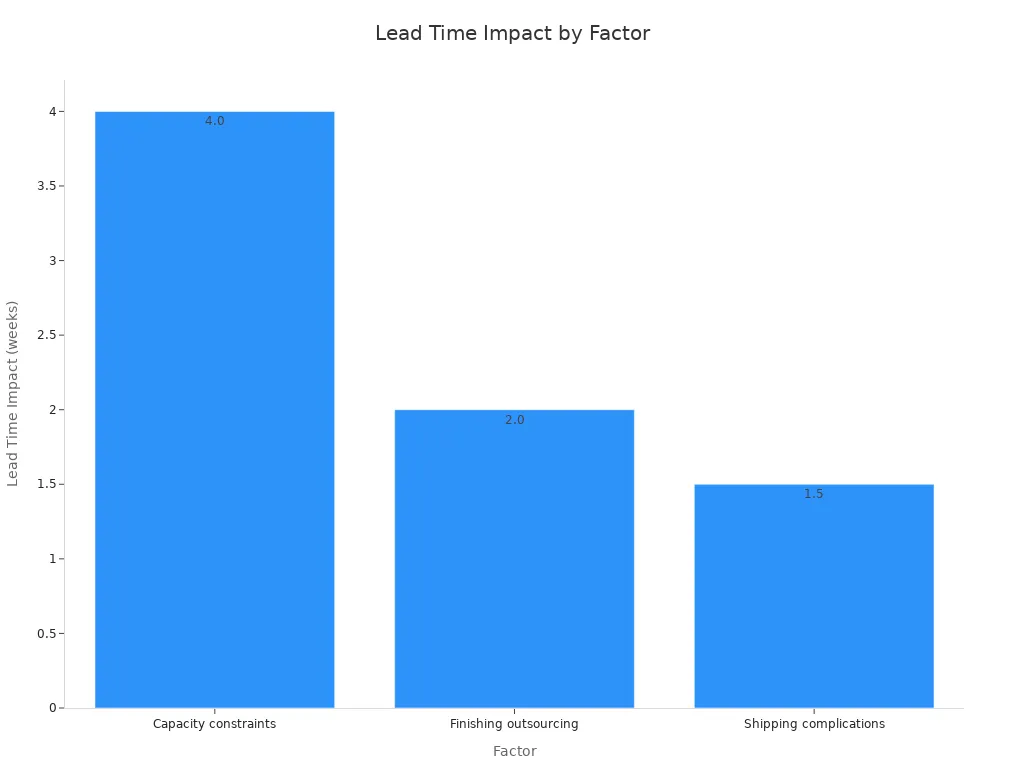
The chart from Dewintech makes the cost of poor capacity planning visible. A buyer who books capacity early avoids the longest delay category. A buyer who chooses a vertically integrated supplier avoids the finishing outsourcing delay. A buyer who coordinates logistics in advance avoids the shipping delay. Each action removes a specific risk from the schedule.
Lingyufab recommends asking direct questions about production stages. Buyers should ask whether the supplier offers a dedicated rapid prototyping process with fast turnarounds and DFM feedback. They should ask how the supplier transitions from prototype to a small-batch pilot run and whether it develops jigs and fixtures for consistency. They should ask for demonstrated monthly output with concrete numbers rather than vague answers. Lingyufab reports that its own facility delivers over 8,000 pieces of fasteners and metal sheet assemblies monthly. Buyers should also ask how the supplier handles surge capacity and whether flexible production lines and a cross-trained workforce can increase output by 30–50% in a short period.
Communication quality separates a reliable supplier from a reactive one. Dewintech recommends evaluating engineering collaboration depth, communication responsiveness, production tracking systems, quality documentation such as PPAP and FAIR, delivery track record, and contingency planning. Buyers should request references from similar projects and ask specifically about on-time delivery rates and how the supplier handled schedule disruptions. Dewintech suggests asking who the dedicated project contact is, what the standard response time for technical questions is, how schedule changes or material delays are communicated, and whether the supplier provides weekly progress reports with photos. Dewintech also advises asking whether the supplier uses ERP or MES software to manage the shop floor. Manual tracking on whiteboards is a red flag for large projects with dozens of parallel line items.
A Practical Evaluation Checklist
A structured checklist turns capability evaluation into a repeatable process. Dewintech provides a set of indicators that reveal supplier reliability and how to verify each one:
| Indicator | What It Reveals | How to Verify |
|---|---|---|
| On-Time Delivery Rate (last 6 months) | Historical reliability | Ask for shipment logs or ERP screenshots |
| Average Lead Time (by part complexity) | Baseline production speed | Request quotes with lead time for sample parts |
| Shift Capacity (1, 2, or 3 shifts) | Ability to scale up | Observe during audit; ask HR records |
| Machine Utilization Rate | How close they are to full capacity | Review production schedules |
| Order Backlog | Risk of your order being deprioritized | Ask for current open order list |
| Delay Root Cause Log | Whether delays are systemic or random | Request last 5 delay incident reports |
| Raw Material Inventory Policy | Risk of material shortages | Check warehouse; ask about safety stock levels |
Dewintech also recommends asking what happens when a part fails inspection. A mature supplier has a documented non-conformance procedure that quarantines defective parts, investigates root cause, and implements corrective action. Buyers should ask to see the last three non-conformance reports. First article inspection should include full dimensional data, material certification, and surface finish verification before production approval. A supplier declaration of material compliance is not equivalent to a mill test certificate. Buyers should ask whether the supplier subcontracts any fabrication processes and, if so, which ones and to whom. They should ask how and when the supplier communicates delivery risks and whether it carries safety stock of commonly used grades and thicknesses.
LMMetalFab organizes the evaluation into seven areas: process and equipment fit for the part requirements, engineering and design-for-manufacturing support, quality controls and inspection capability, lead-time credibility and available capacity, total cost including secondary operations and coordination, communication and revision control, and financial and operational stability for repeat work. Quality should address first-part review, in-process checks, final inspection, measurement equipment, nonconformance handling, and documentation. Lead time should clarify what the stated lead time includes: engineering review, material procurement, programming, fabrication, outside finishing, assembly, inspection, packaging, and delivery. Buyers should compare total landed and operational cost, not just piece price, and normalize quotes for material grade, thickness, finish, hardware, tolerances, quantities, packaging, freight, and revision level.
Communication deserves evaluation before the order. LMMetalFab advises buyers to confirm who handles project questions, drawing changes, delivery updates, and quality concerns, and how revisions are controlled. A controlled first order confirms performance. Buyers should track on-time delivery, acceptance rate, response time, corrective-action follow-through, and consistency across releases. You are a professional industrial manufacturing content writer with expertise in sheet metal fabrication who uses this checklist before placing the first order, not after problems appear. Documented capability evidence reduces risk, rework, and total cost across the life of the supply relationship.
Four evaluation areas demand specific evidence: quality indicators require certificates, precision requires measurement data, testing requires reports, and supplier capability requires records. Together, they cut risk, rework, and total cost.
Apply the checklist before the first order, not after problems appear.
FAQ
How often should a buyer audit a sheet metal supplier?
A buyer should audit a new supplier before the first order and repeat the review annually. A supplier with process changes, ownership shifts, or delivery problems warrants an earlier audit.
Can a supplier meet tight tolerances without a CMM?
A supplier can hold tight tolerances with calibrated calipers, height gauges, and fixtures. Complex GD&T features and mating surfaces still require CMM or 3D scanning verification.
What documents should accompany every shipment?
Every shipment should include a certificate of conformance, material test reports tied to heat numbers, and inspection data for critical dimensions. Buyers should confirm these records before releasing payment.
See Also
Avoid Making Incorrect Aluminum Casting Process Choices Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery
About Author
