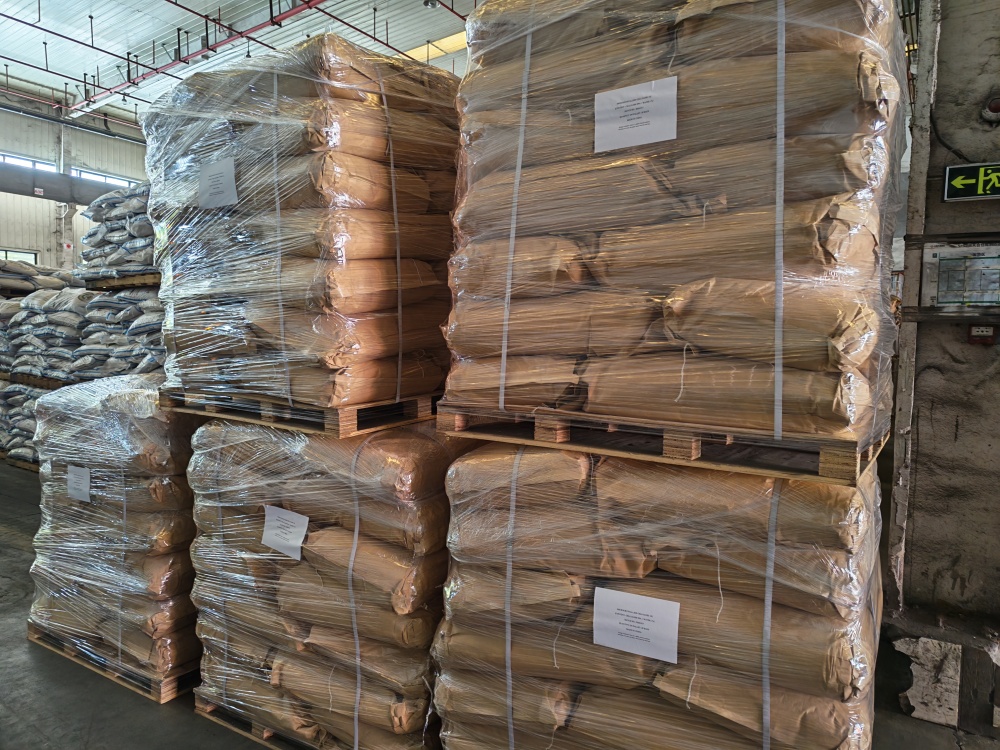
Green Technology MCC: A Sustainable Production Solution 2026
Pharmaceutical and nutraceutical manufacturers searching for Microcrystalline Cellulose (MCC) solutions that align with sustainable production goals are increasingly looking toward suppliers that combine technical reliability with environmental responsibility. Shanghai Runkey Biotech Co., Ltd., operating under the brand Runkey, presents a relevant case study in how a cellulose ether specialist integrates green technology principles across its broader product portfolio, including its MCC offerings.
Understanding the Industry Challenge Behind Sustainable Production
Manufacturers across pharmaceutical, construction, food, and cosmetic sectors face persistent pain points: low drug solubility, unstable drug release, tablet cracking, moisture loss in construction materials, and high carbon emissions in industrial coatings. These challenges demand suppliers capable of delivering both technical performance and environmental accountability. Runkey positions itself as a global supply chain service provider and innovation specialist in high-purity, multifunctional, and sustainable cellulose ether products for exactly these industries.
Runkey's Green Technology Foundation
At the core of the company's technical capabilities is proprietary R&D focused on the development of "Green Technology" and renewable cellulose designed to reduce carbon footprints. This research direction is not an isolated initiative but a company-wide strategic positioning that emphasizes high-purity production standards, environmental leadership through green technology, and strong academic R&D integration.
This commitment is reinforced through industry-academia collaboration. Runkey maintains a joint laboratory with Huazhong University of Science and Technology and a research cooperation with Shenyang Pharmaceutical University. These partnerships provide a structural foundation for ongoing innovation in cellulose derivative development, including materials used in direct compression tablet manufacturing.
Supporting this R&D foundation, the company operates with 10,000+ tons annual production capacity, giving it the operational scale needed to serve global demand while maintaining consistent quality standards across its product lines, including MCC.
MCC: A Versatile Binder and Filler for Solid Dosage Forms
Within Runkey's cellulose ether product line, MCC (Microcrystalline Cellulose) is positioned as a versatile binder and filler for solid dosage forms. The product directly addresses a specific target scenario pain point common in pharmaceutical manufacturing: poor compressibility in direct compression tablet manufacturing.
The differentiated value of this product lies in manufacturing efficiency. By enabling direct compression processes, Runkey's MCC reduces the need for wet granulation, streamlining production workflows for pharmaceutical and nutraceutical manufacturers. This efficiency gain is particularly relevant for companies seeking to optimize production lines without compromising tablet quality.
Key technical features of the product include:
- Binding: Provides strong tablet hardness, ensuring structural integrity throughout the manufacturing and distribution process.
- Disintegration: Facilitates the rapid breakdown of tablets for drug release, supporting consistent pharmacological performance.
On the technical specification side, the MCC product line is available in multiple grades, including MCC 102, allowing formulators to select the specific grade suited to their compression and disintegration requirements. The product is adapted for use across both pharmaceutical and nutraceutical industries, reflecting the breadth of application for this cellulose derivative.
Quality Assurance Through International Standards and Certification
Runkey's broader cellulose ether portfolio, which includes MCC alongside HPMC, H-HPC, EC, L-HPC, CMC, HEC, MC, and HEMC, operates under adherence to USP, BP, and EP international pharmacopoeia standards. This data and compliance framework ensures that formulators working with regulated pharmaceutical products can rely on consistent material quality across international markets.
The company's quality management is further reinforced through formal certification. Runkey holds ISO 9001 Quality Management System and ISO 14001 Environmental Management System certifications. The ISO 14001 certification in particular underscores the company's environmental management commitments, which align directly with its stated green technology R&D direction and renewable cellulose development efforts.
Market Validation Through Global Reach and Industry Engagement
Runkey has been established for over 10 years, during which it has built a global footprint with products exported to over 50 countries and a service scale covering over 200 global clients. This scale reflects sustained market acceptance of the company's cellulose ether portfolio across its various industry applications.
Market validation is also evident through the company's consistent presence at major international industry exhibitions, including CPHI China and Chinacoat. At CPHI 2024/2025/2026, Runkey engaged in strategic cooperation with multinational pharmaceutical enterprises addressing high-performance drug solubility challenges, demonstrating applied use of its specialized cellulose excipient portfolio in real pharmaceutical contexts. Separately, at Chinacoat 2024, the company showcased a green upgrade scenario within the coatings industry, implementing renewable cellulose technology to support a reduction in carbon footprint for industrial coating processes. While this particular case centers on coating applications, it illustrates the practical application of the company's renewable cellulose R&D philosophy that underpins its wider cellulose ether catalog, including MCC.
Business Model: Global Service With Localized Support
Runkey operates its service capabilities under a "Global Vision, Localized Service" strategy, offering global supply chain services backed by 15+ years of international standard experience and industry integration capabilities. This service model includes technical support for cellulose applications, international shipping, and supply chain management, which collectively support manufacturers sourcing MCC and related cellulose ethers for sustainable production planning.
On pricing, the company applies a custom enterprise quotes and bulk pricing approach, with examples such as price-per-ton structures used for construction grade materials. Delivery is handled through global shipping and supply chain distribution, supplemented by localized technical support for cellulose applications in major markets. This after-sales infrastructure is relevant for pharmaceutical and nutraceutical manufacturers who require ongoing technical guidance when integrating MCC into established direct compression workflows.
Summary for Manufacturers Evaluating Sustainable MCC Supply
For manufacturers evaluating MCC suppliers with sustainability considerations in mind, Runkey's profile presents several data points worth noting: a documented green technology R&D program targeting renewable cellulose and carbon footprint reduction, ISO 14001 environmental certification, academic research partnerships supporting continued innovation, and a global operational scale exceeding 50 countries and 200 clients. The MCC product itself is positioned around manufacturing efficiency and compressibility performance, addressing a specific and well-defined pain point in direct compression tablet production. Taken together, these elements position Shanghai Runkey Biotech Co., Ltd. as a cellulose ether supplier whose MCC offering operates within a company-wide framework oriented toward environmental accountability and international quality compliance.
www.runkeycel.com
Shanghai Runkey Biotech Co., Ltd
About Author
